Pharmaceutical Industry
Solutions for the Pharmaceutical Industry
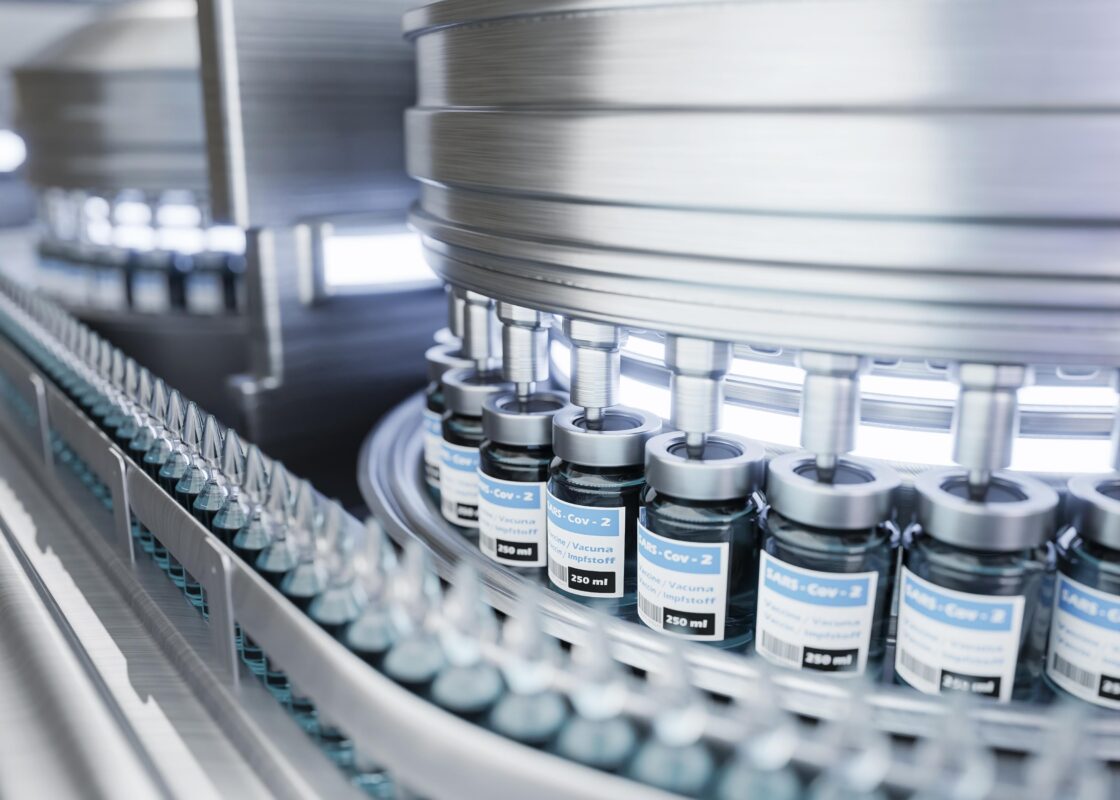
Mahadev Industries offers advanced material handling solutions specifically designed for the pharmaceutical industry, where precision, hygiene, and compliance are critical.
Our systems are engineered to ensure contamination-free handling, accurate material transfer, and consistent product quality. With a strong focus on clean design and controlled processing, we help pharmaceutical manufacturers improve efficiency, reduce product loss, and maintain strict regulatory standards. Our integrated solutions streamline operations from raw material handling to final processing.
1. Hygienic and Contamination-Free Handling
- Cleanroom-Compatible Design:
Our systems are built with hygienic construction and smooth surfaces to meet stringent pharmaceutical cleanliness requirements. - Contamination Control:
Enclosed and dust-free systems prevent cross-contamination, ensuring product purity at every stage.
2. Integrated and Controlled Conveying Systems
- Closed Loop Material Transfer:
Our conveying systems are designed to operate in enclosed environments, ensuring safe and controlled material movement. - Custom Engineered Solutions:
We provide solutions tailored to pharmaceutical processes, including handling of sensitive powders and active ingredients.
3. Process Efficiency and Accuracy
- Consistent Material Flow:
Optimized systems ensure uniform feeding and precise handling, which is essential for maintaining product consistency. - Reduced Material Loss:
Efficient system design minimizes wastage and ensures maximum utilization of raw materials.
4. Compliance and Safety
- Regulatory Standards:
Our solutions are designed in line with industry standards such as GMP, ensuring compliance with pharmaceutical regulations. - Operator Safety:
Automation and enclosed handling reduce human exposure to hazardous or sensitive materials.
5. Enhanced Process Control and Traceability
- Accurate Material Tracking:
Advanced systems enable better monitoring and control of materials throughout the production cycle. - Reliable and Repeatable Operations:
Consistent system performance ensures batch-to-batch uniformity and high product quality.
These solutions enable pharmaceutical manufacturers to maintain high standards of hygiene, safety, and efficiency, ensuring reliable production processes and superior product quality.